Industries / Food Processing
Food processing automation: Packaging and end-of-line solutions.
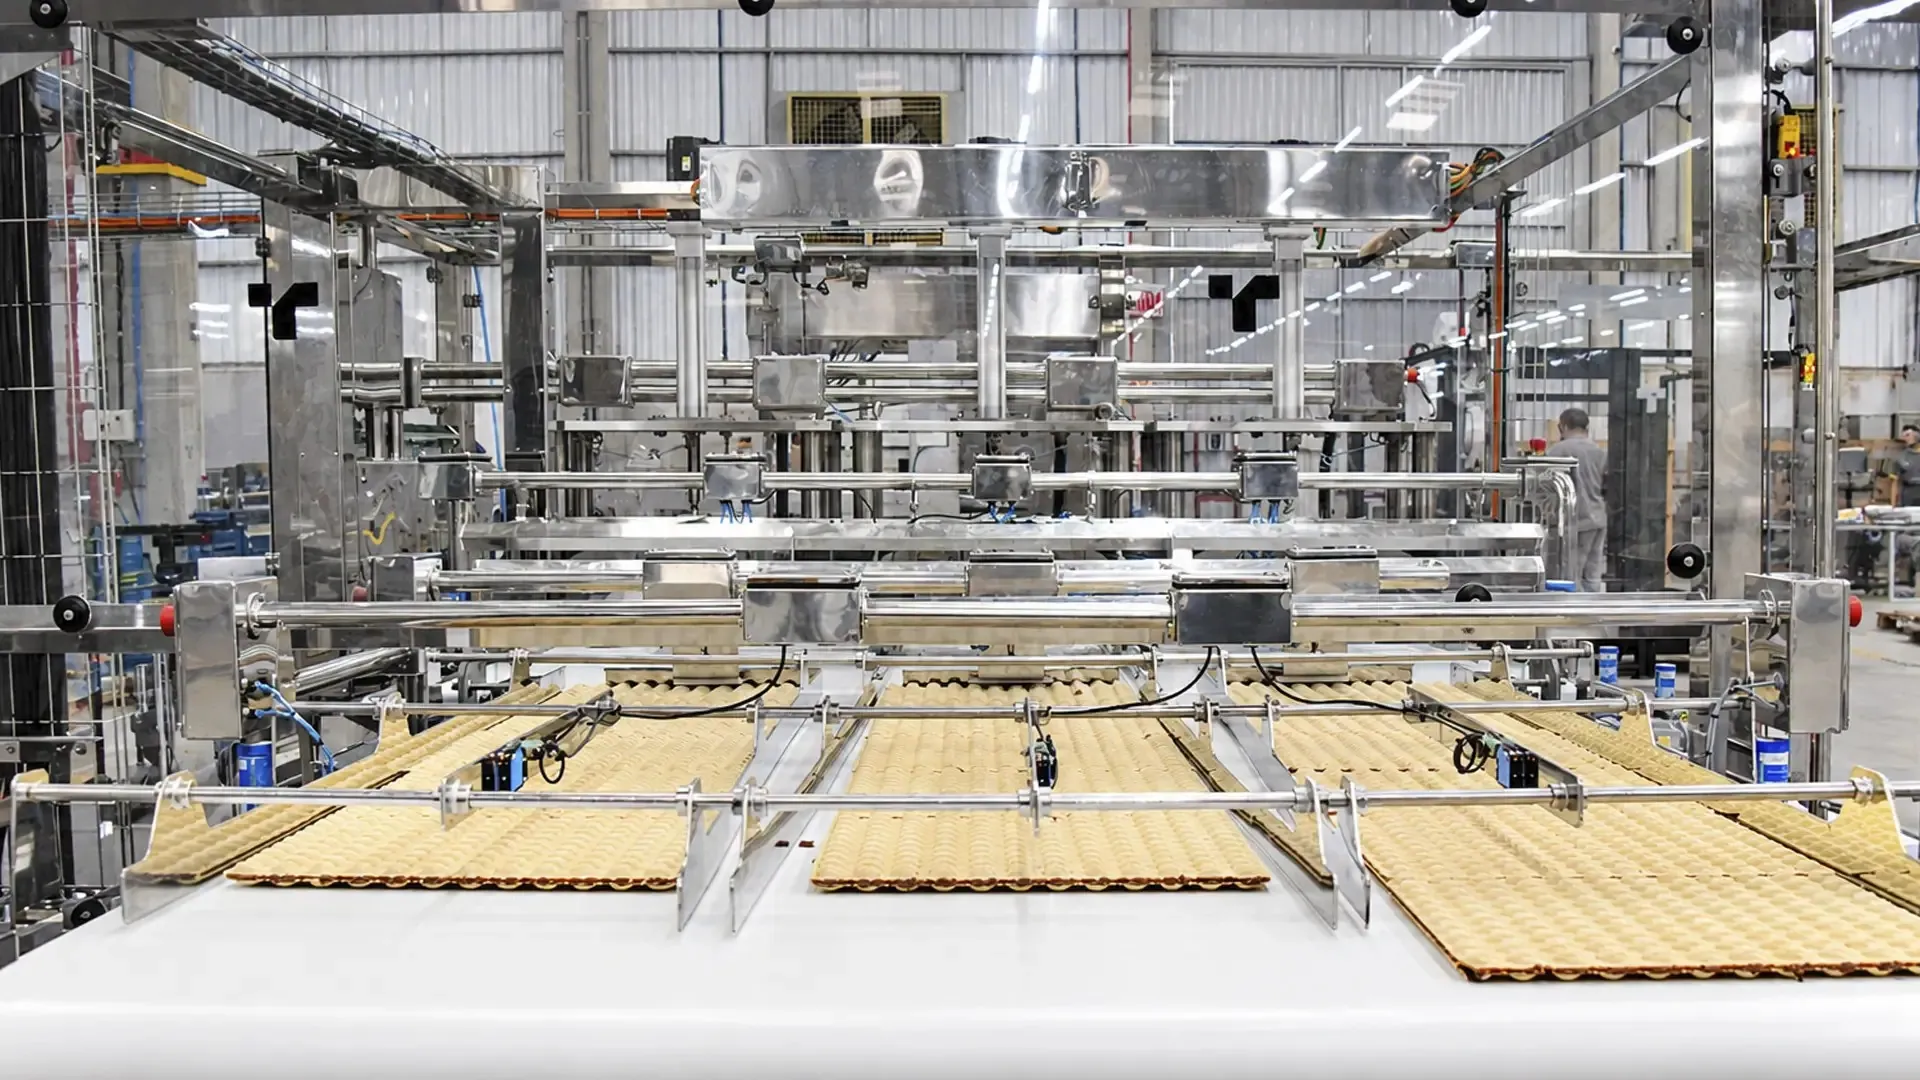
Robotic palletizing, case packing and conveyor systems after primary packaging, matched to each food line's rate and floor space.
Food processing automation from TRF Industrial Automation means robotic palletizing, case packing and conveyor systems at the end of the line, after primary packaging. TRF is a U.S.-based company and part of the Torfresma Group, and it supports food manufacturers across the United States with end-of-line equipment engineered for each plant.
Custom engineering
Solutions engineered for your production requirements.
Turnkey integration
From system design through installation and startup.
High reliability
Built for continuous operation.
U.S. support
Technical support for customers across the United States.
Lifecycle support
From startup to long-term performance.
Key facts about food processing automation
| Topic | What TRF offers food processing manufacturers |
|---|---|
| Scope | Robotic palletizing, case packing and conveyor systems at the end of the line, after primary packaging |
| Typical packages | Cases, bags, trays, cartons, cups and tubs |
| Platforms | TRFCobot, TRFCompact, TRFSpeed, TRFSubzero, TRFRapidpack, TRFOnepack, TRFDroppack, TRFIntraflow and TRFCleanflow, plus custom palletizers |
| Delivery model | One partner accountable for the agreed scope of engineering, manufacturing, controls, installation and commissioning |
| Coverage | Food Processing manufacturers across the United States |
What does food processing automation include at the end of the line?
TRF automates three jobs after primary packaging, and each one is sized to the line it serves instead of being sold as a fixed package.
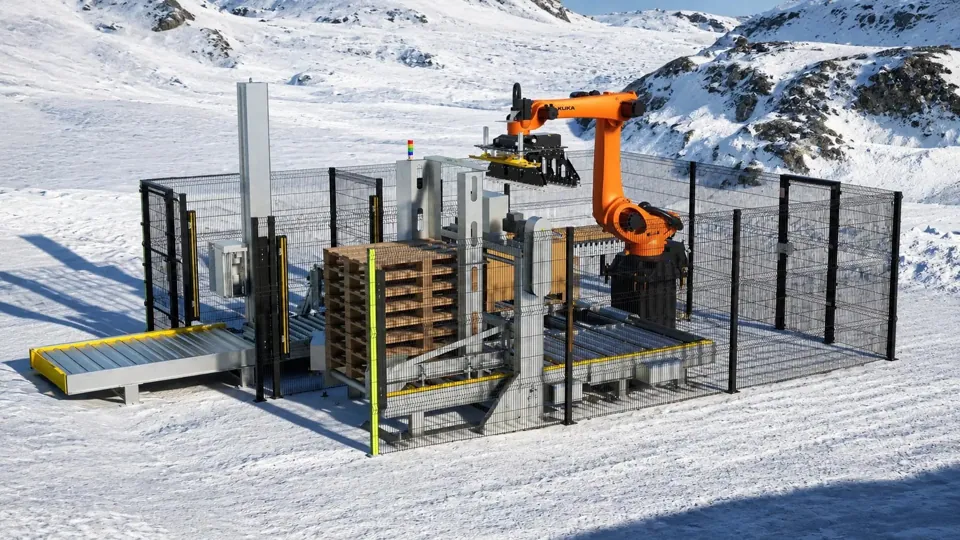
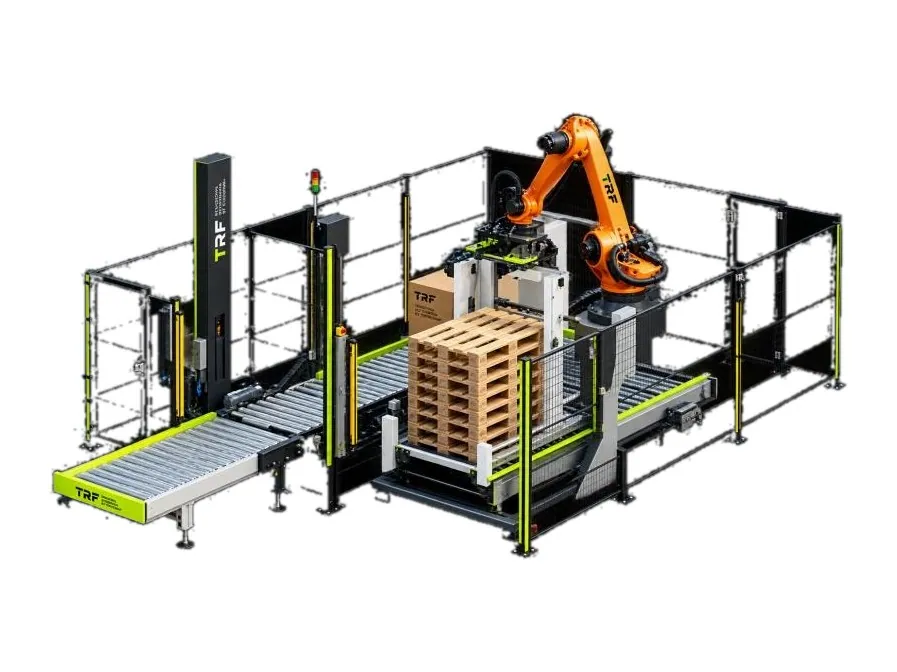
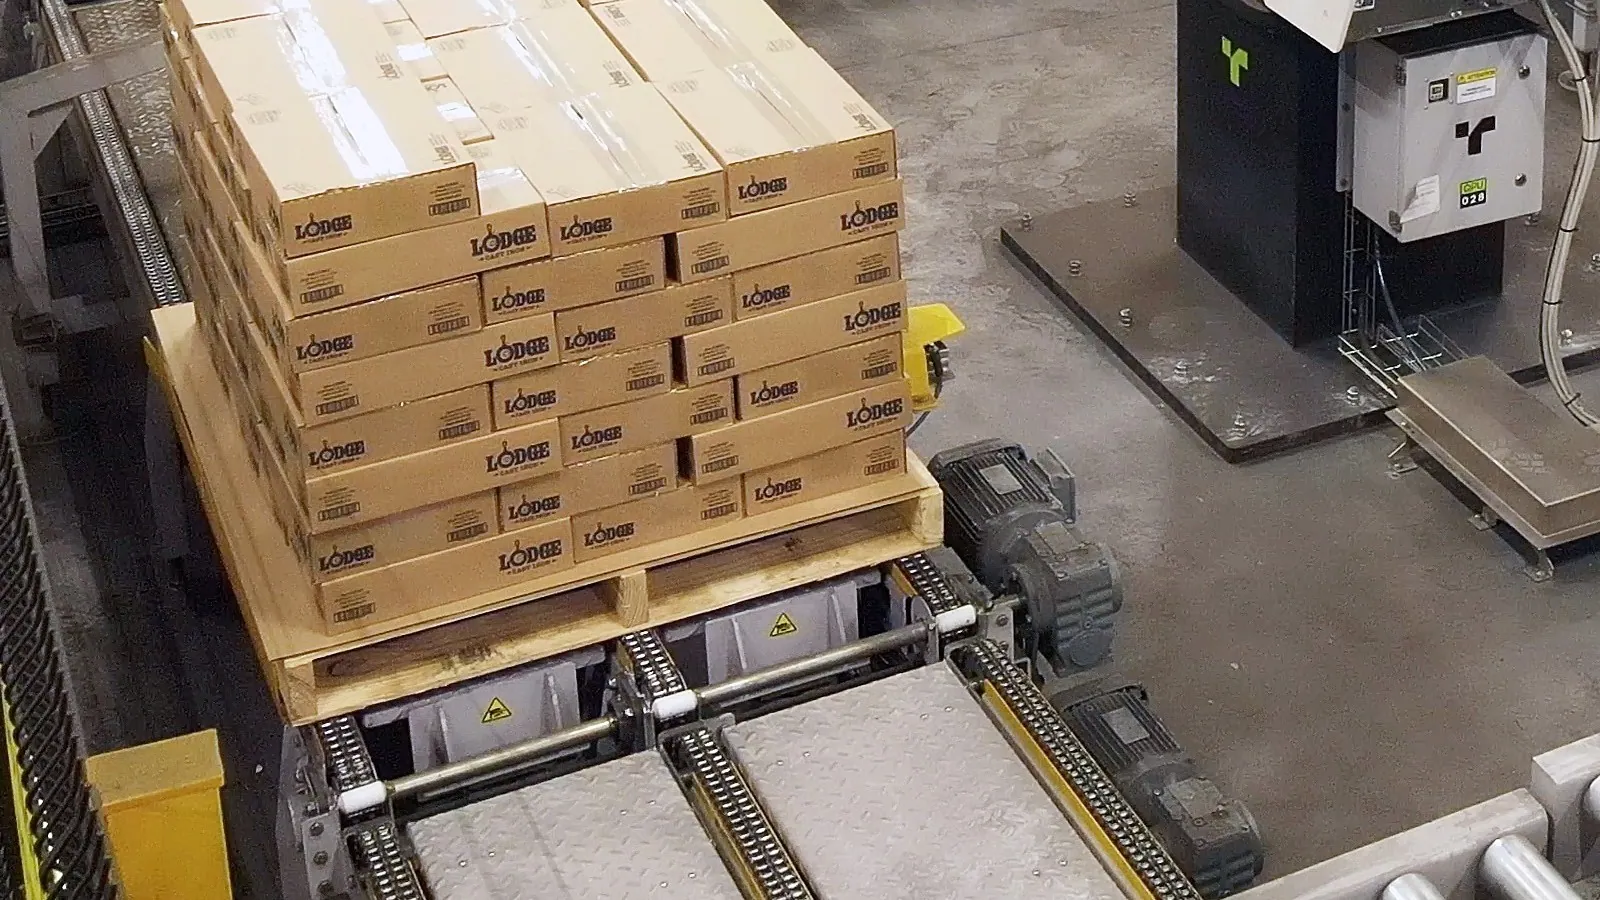
Robotic palletizing. Cases, bags and trays reach the palletizer from the case packer or straight from the line, and a robot builds the pallet in the pattern the customer expects. TRF offers collaborative, compact and high-speed palletizing, plus a cold-area option for frozen products. See the robotic palletizing page for the full range of platforms.
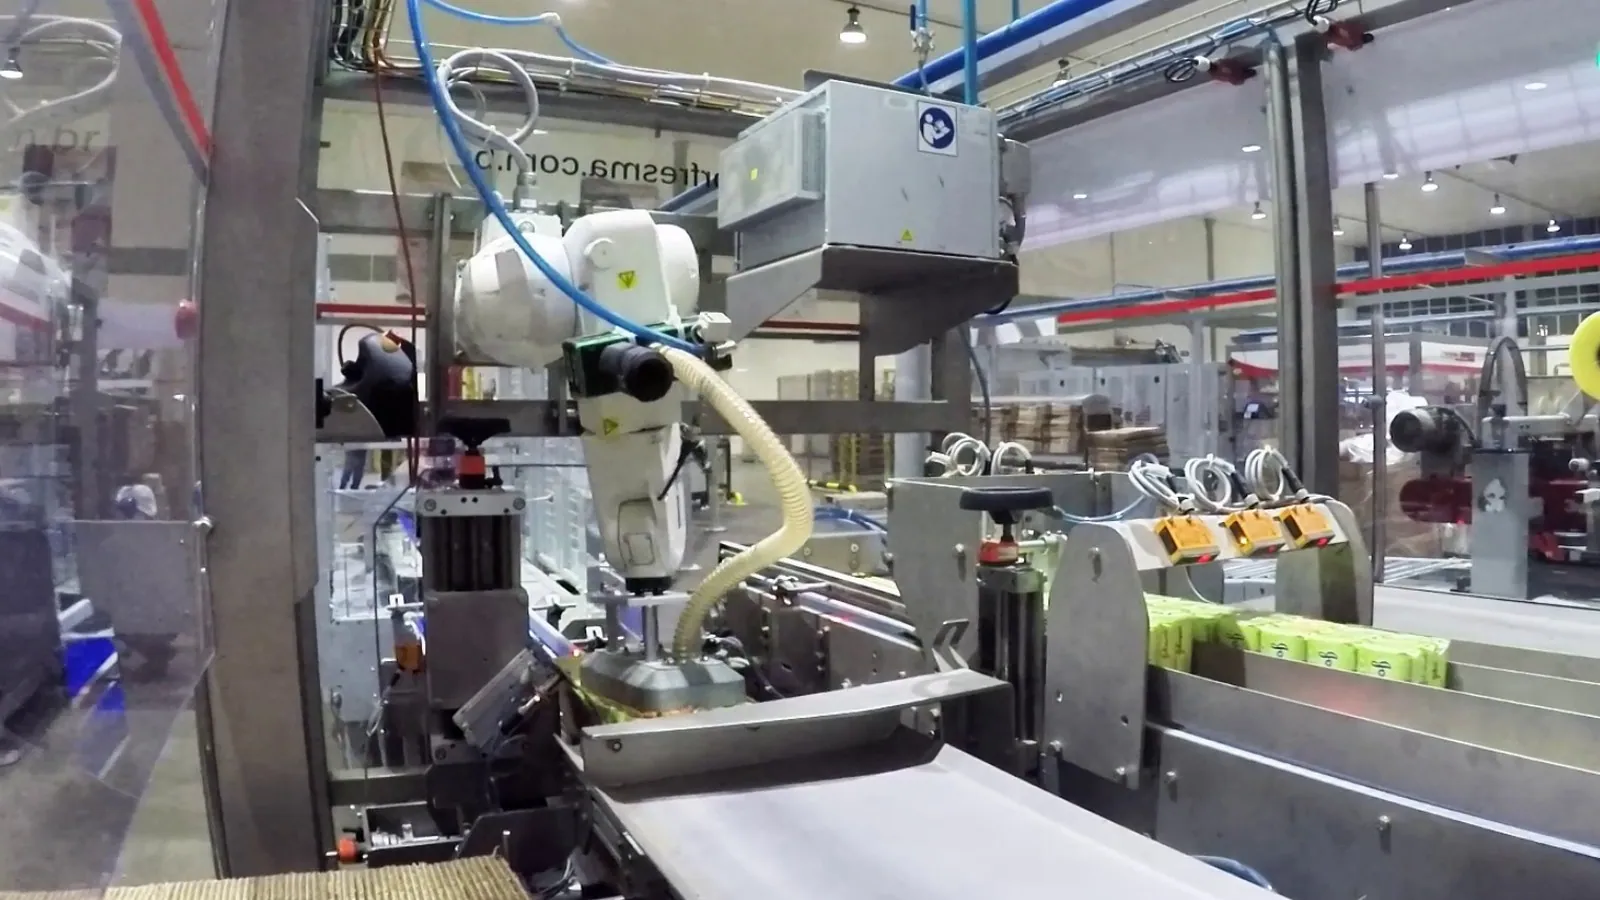
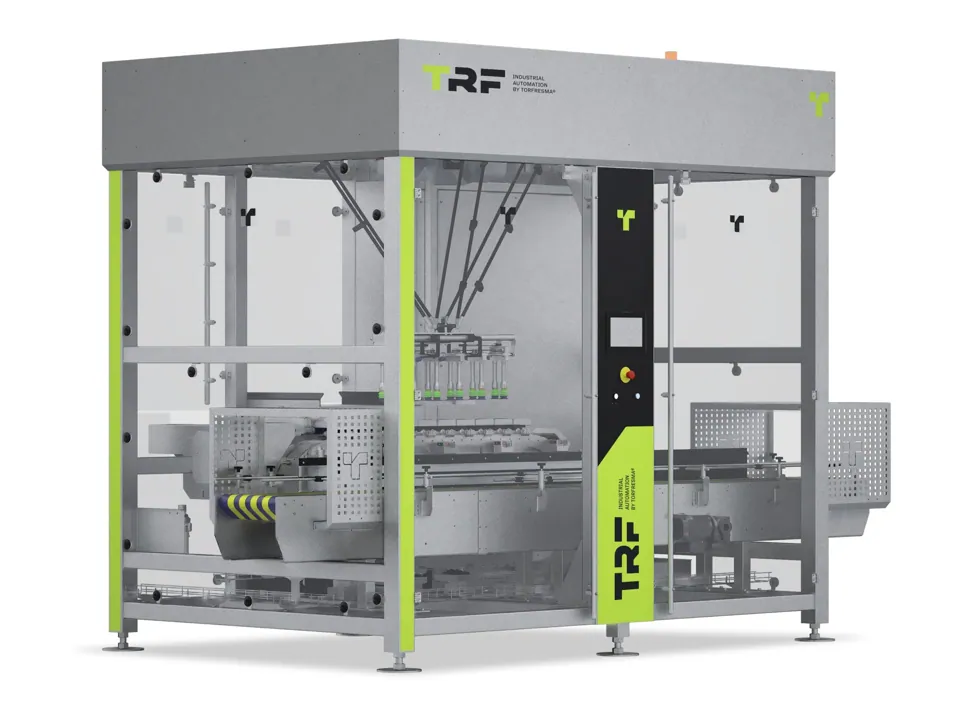
Case packing. Packaged food goes into shipping cases by robot, by an integrated machine that forms, packs and seals, or by gravity loading for bags and pouches. TRF reviews all three options for each product, because line setup and speed often decide the platform more than the package alone. See the case packing page for the three case packer platforms.
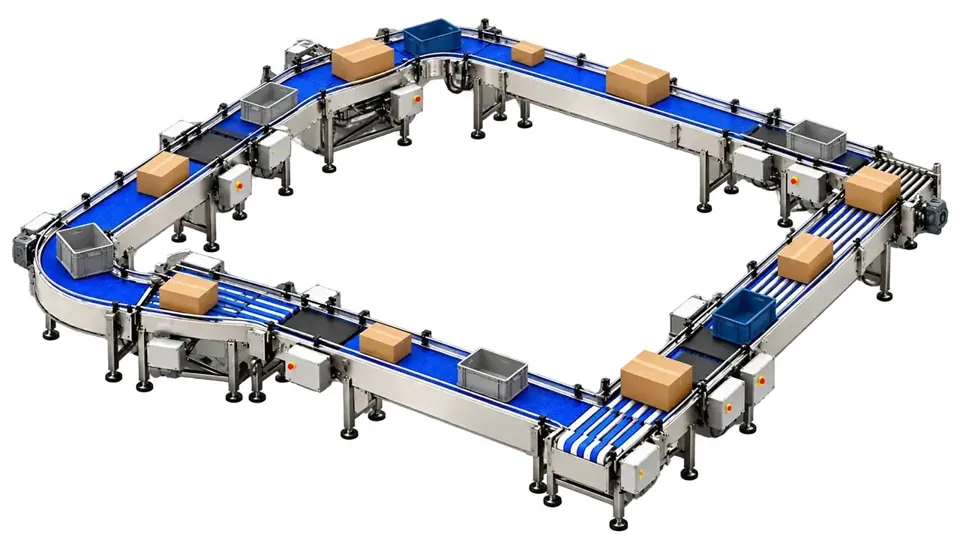
Conveyor systems. Conveyors link the case packer, the buffer and the palletizer, with accumulation, merging, diverting and elevation as the plant layout requires. Where the project includes a hygienic food conveyor for open product, TRF coordinates it with the case conveying that follows. The case conveyor systems page describes the modules.
How TRF evaluates a food processing line
Food lines differ in package, speed and space, so TRF does not start from a fixed configuration. A Sales Engineer reviews six points of the line before recommending platforms:
- Application. What is packed or palletized (cases, bags, trays, cartons, cups and tubs), its dimensions, how it arrives from primary packaging and how it has to leave the cell.
- Speed. The line rate in products per minute or cases per minute, today and at the planned growth. The rate points to a cobot, a compact industrial robot or a high-speed system.
- Weight. The weight of each case, bag or pail, which sets the gripper and the platform class.
- Pallet pattern. The pallet size, the layer pattern, the stack height and any requirement from the customer receiving the pallet.
- Space. The floor area and ceiling height after primary packaging, including plants where the new cell has to fit around current equipment.
- Integration. The conveyors, controls and machines already in place, and the point where TRF connects to each of them.
Platforms for food processing automation
The platforms that usually come up in food processing depend on how many products share a line and how much room the plant has.
- Palletizing. TRFCobot fits lower-speed, high-mix lines that still palletize by hand, TRFCompact fits plants with limited space, and TRFSpeed fits high-volume or multi-line operations. TRFSubzero applies when pallets are built in areas below 32°F.
- Case packing. TRFRapidpack suits many SKUs and delicate items, TRFOnepack erects, packs and seals the case in one machine, and TRFDroppack suits bags and pouches that tolerate controlled gravity loading.
- Conveying. TRFIntraflow moves, accumulates and routes closed cases. TRFCleanflow is reviewed when the application needs a hygienic conveyor for open food.
Typical ranges for commercial screening. TRF engineering confirms final capacity for each application (product, end-of-arm tool, pallet pattern, reach and process).
When an application falls outside the standard platforms, TRF engineers a custom palletizer around your products and throughput.
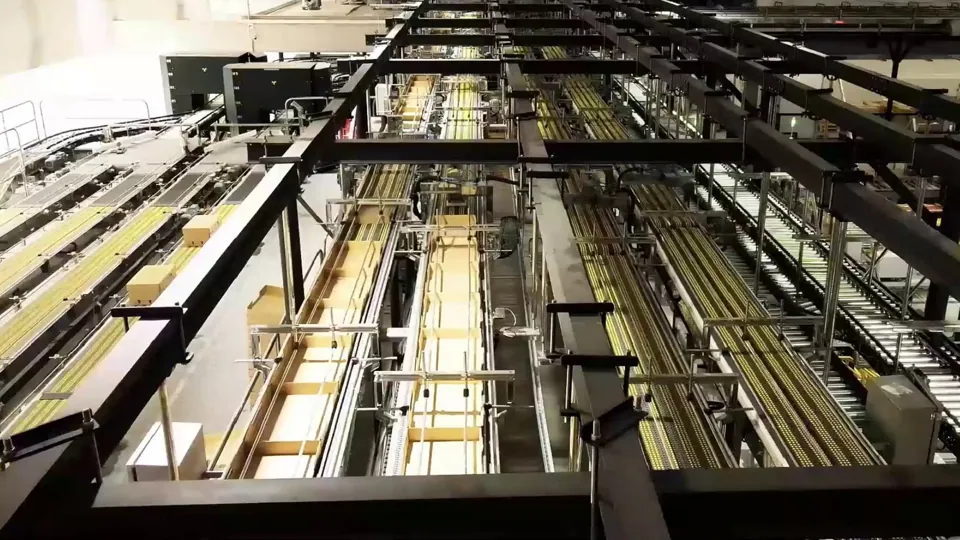
How a food processing project moves from first call to commissioning
A TRF project follows the same path in every segment, so you know what to expect from the first conversation:
- Information. You send the package formats, case sizes, line speeds, shifts and a drawing or photos of the space after primary packaging.
- Screening. A Sales Engineer reviews the six points above and screens the platforms that fit the line.
- Layout and proposal. TRF shows how the equipment fits in your plant and defines the scope that the proposal covers.
- Engineering and manufacturing. TRF engineers the mechanics and the controls as one system for the agreed scope.
- Installation and commissioning. The same partner installs and commissions the system, so one team is accountable for the project.
Start with the information you already have. A partial drawing and a list of products are enough for a first conversation with a Sales Engineer about food processing automation.
Projects and videos for food processing
TRF gathers projects and videos of applications in food processing and in neighboring segments. During the evaluation, the Sales Engineer shows the examples closest to your packages, line rate and space, so you can see how a similar end of line is arranged before you decide.
Questions
Frequently asked questions
What should a food plant automate first at the end of the line?
Start where manual work is heaviest or where the line stops most often. For many plants that is palletizing, because lifting cases all shift is demanding and hard to staff. For others it is case loading. A TRF Sales Engineer reviews the whole end of the line and proposes a sequence, so the first step fits the full system later.
How can a food plant with many SKUs keep changeovers short?
Recipe-based pallet patterns and pack patterns let the system switch products from the operator panel instead of by mechanical adjustment. TRF reviews your SKU list, case sizes and run lengths to decide which platforms store the number of recipes you need.
Where does TRF start if my line already has primary packaging machines?
TRF connects at the discharge of the existing machine. The Sales Engineer asks for the product, the exit orientation and the rate, then engineers the conveyor, case packer or palletizer that receives it. The primary packaging machine stays with its supplier.
How do I know a food line is ready for a robotic palletizer?
Common signs are cases that are hard to staff for, lifting that slows the line at peak shifts, and a pallet area that limits shipping. The Sales Engineer reviews the rate, the case weight and the space, and tells you whether a cobot, a compact cell or a high-speed system fits. The palletizing ROI calculator helps you size the savings.
Should a food plant use a dedicated palletizing cell or a centralized multi-line system?
A dedicated cell suits a line that runs on its own, sitting next to its case packer. A centralized system suits several lines that can share one palletizing area, with conveyors merging the cases. TRFSpeed scales from one to the other, and TRF validates the combined rate for each plant.
Start your food processing automation project
Food processing automation works when every step after primary packaging is sized for the same line: the case packer for the products per minute, the conveyors for the flow and buffer, and the palletizer for the cases per minute, load and floor space. Send your package formats, case sizes, line speeds and shifts, and a TRF Sales Engineer will screen the platforms that fit and describe the integrated line. Other segments are listed on the industries page.
Next step
Keep your production running.
Tell us about your products, rates and floor space. A TRF Sales Engineer answers with the platform, the layout and the next step for your line.