Industries / Beverage
Beverage packaging automation and end-of-line solutions.
Robotic palletizing, case packing and conveyor systems at the end of the beverage line, after primary packaging.
Beverage packaging automation from TRF Industrial Automation covers robotic palletizing, case packing and conveyor systems at the end of the line, after primary packaging. TRF Industrial Automation is a U.S.-based company and part of the Torfresma Group, and it works with beverage producers that want the cases, trays and bundles leaving the packing area conveyed, buffered and palletized by automation.
Custom engineering
Solutions engineered for your production requirements.
Turnkey integration
From system design through installation and startup.
High reliability
Built for continuous operation.
U.S. support
Technical support for customers across the United States.
Lifecycle support
From startup to long-term performance.
Beverage packaging automation solutions: What TRF automates
TRF Industrial Automation delivers beverage automation in three steps at the end of the line. Each one is evaluated for your products, rates and plant, and each one can be a project on its own or part of an integrated system. The typical package is cases, trays and bundles, and TRF confirms the fit for each real product.
Robotic Palletizing
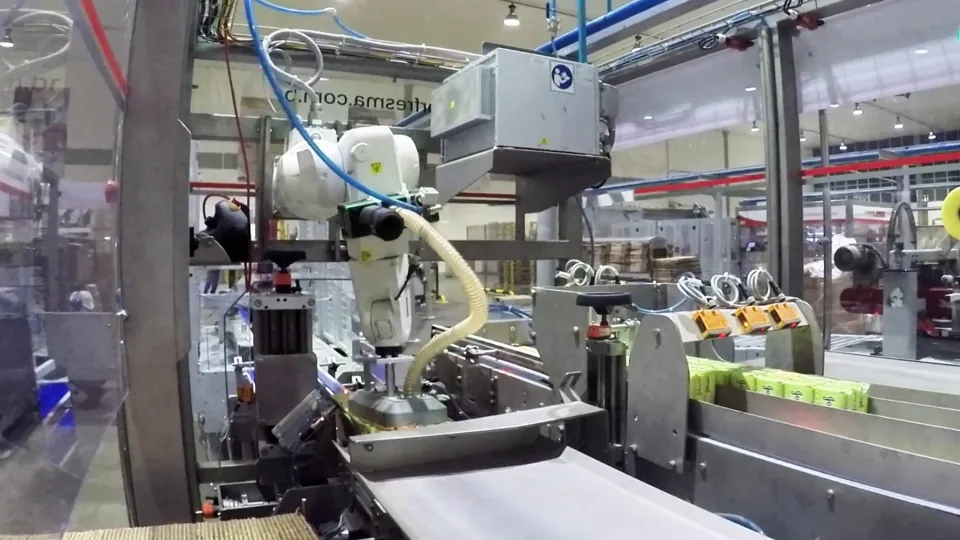
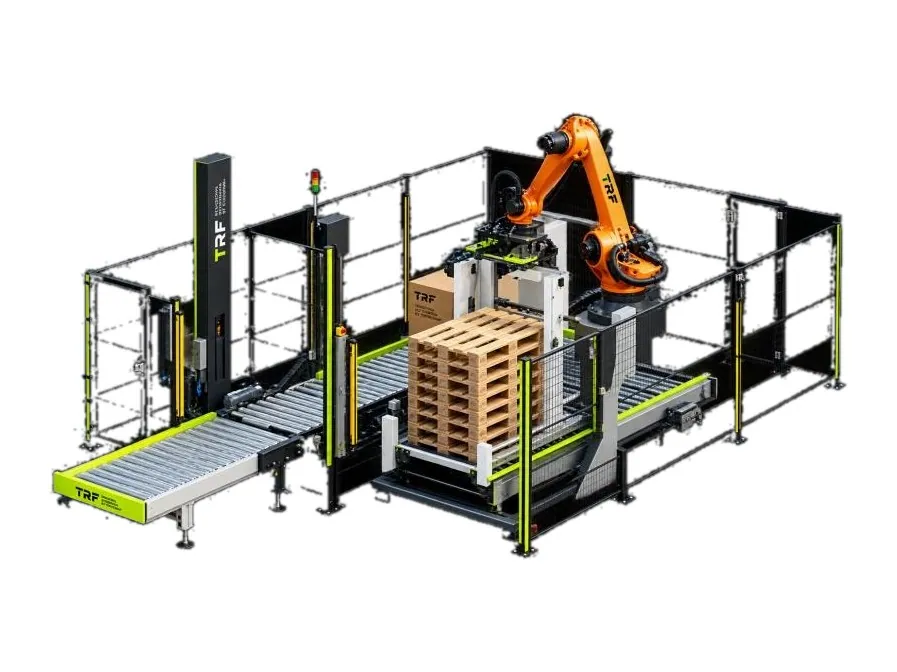
Robotic palletizing replaces manual stacking with a robot that builds stable pallets from stored patterns. In beverage palletizing, the robot builds pallets from the cases, trays and bundles you run. TRF offers the TRFCobot collaborative palletizer, the TRFCompact compact industrial cell and the TRFSpeed high-speed palletizer, plus a custom palletizer when the unit, rate or layout falls outside the standard platforms. The robotic palletizing page compares them.
Case Packing
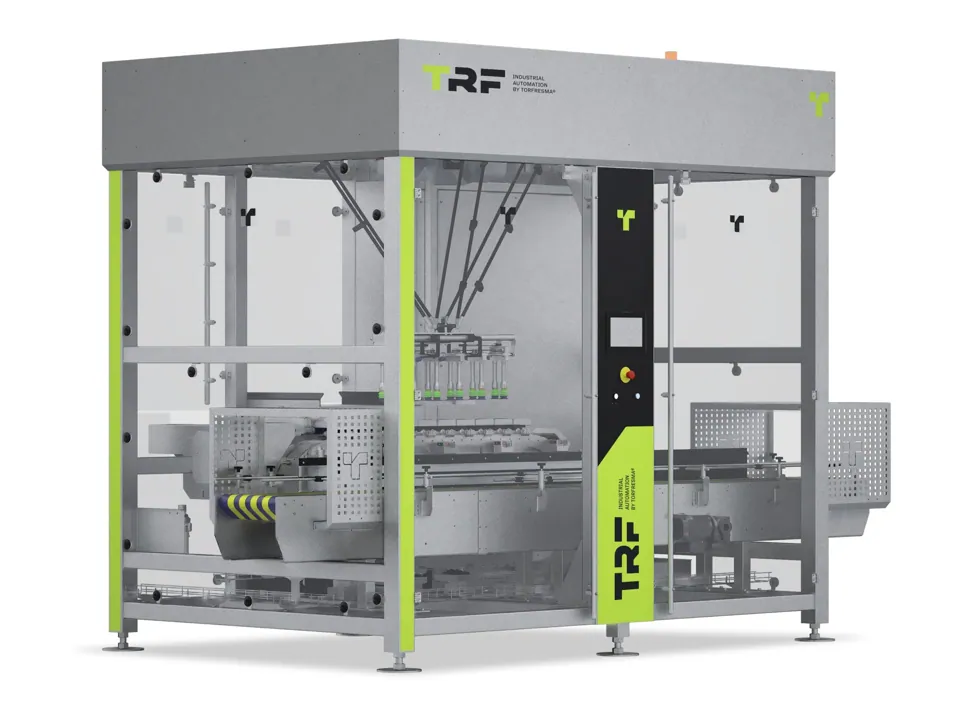
Case packing places packed product into shipping cases. TRFRapidpack is the robotic option, TRFOnepack erects, packs and seals in one machine, and TRFDroppack loads by gravity. The case packing page explains how to choose among them.
Conveyor Systems
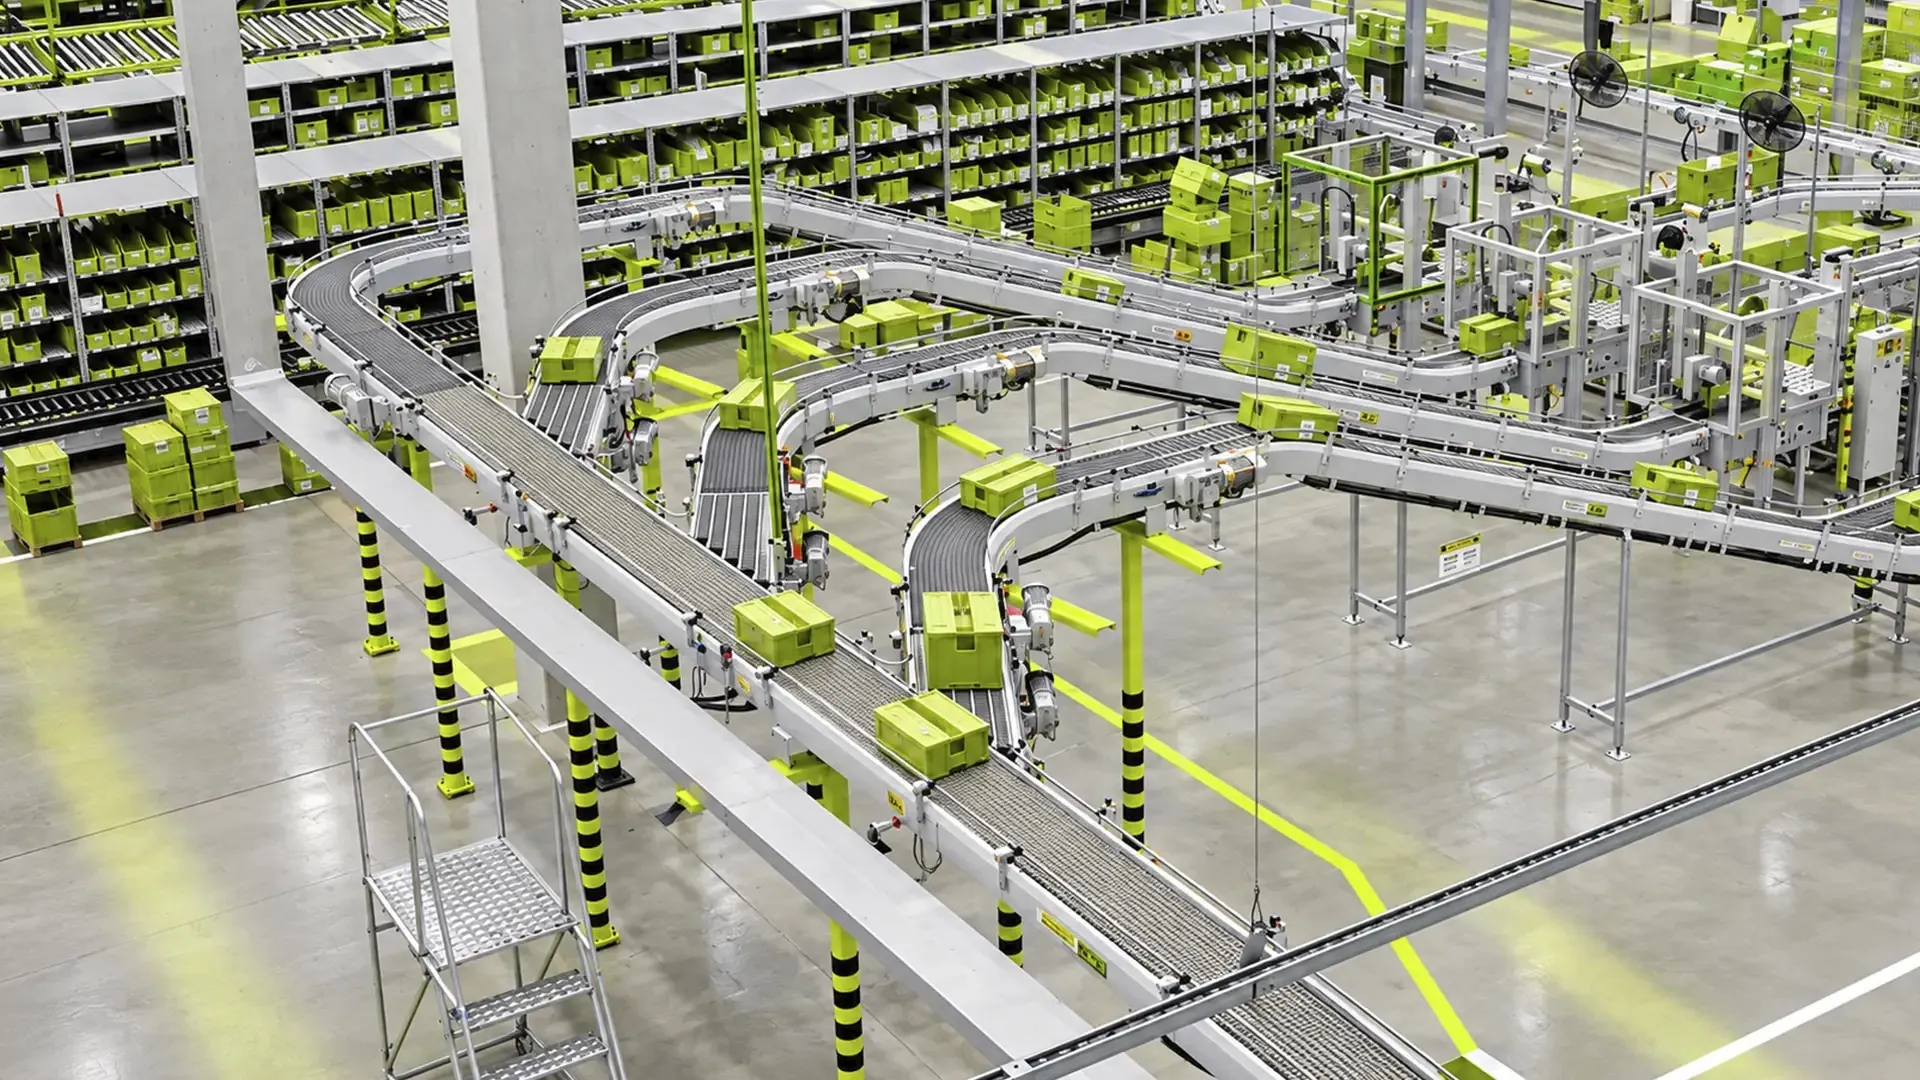
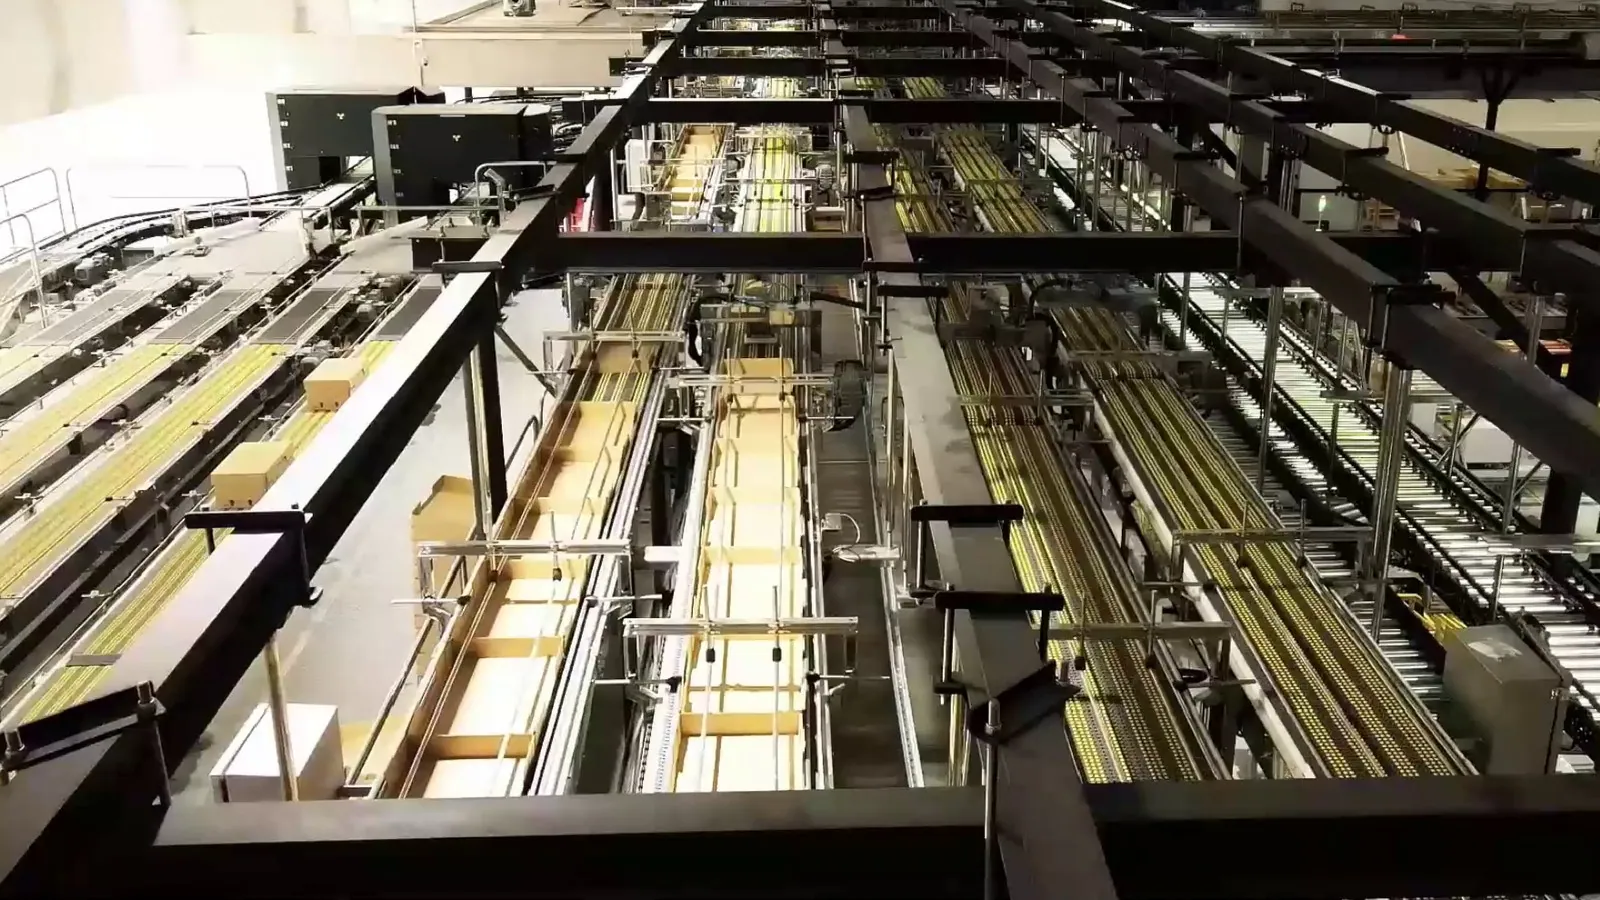
TRFIntraflow conveys, accumulates, merges and diverts cases between the packer, the palletizer and the next area. Where the area calls for hygienic design, TRFCleanflow is evaluated per application.
How TRF evaluates a beverage line
Beverage lines often run at high rates and share a palletizing area between several lines, so buffering, line rate and pallet stability weigh heavily in the review. A TRF Sales Engineer reviews the line with you and covers the same points for every project:
- Application: the products, packages and cases you run today and plan to run.
- Line speed: the rate in packs or cases per minute, including peaks.
- Weight: the weight of the heaviest and lightest case or unit.
- Pallet pattern: pallet size, layer pattern and stacking height.
- Space: the floor area, ceiling height and access available at the end of the line.
- Integration: how the new equipment connects to the machines, controls and conveyors already in place.
The result is a recommendation of which platforms fit, in which order to phase them, and what an integrated project would include.
One partner for the whole end of the line is often the simplest way to run the project. When the case packer, the conveyors and the palletizer are engineered, controlled and started up together, the handoffs between them are designed once, and one team answers for the agreed scope. TRF can also start with a single step, such as the palletizer, and leave room for the other steps to be added later.
What to Send for a First Review
The review starts from your real beverage line, so the more specific the information, the more precise the first recommendation:
- A list of products and package formats, with case sizes and weights.
- Target rates, shifts per day and expected growth.
- Pallet size and pattern, and any customer requirements for the pallet.
- Photos and a rough layout of the end of the line, with the floor space available.
- The equipment already in place that the new system must connect to.
Platforms that often join a beverage project
Any of the nine TRF platforms can be part of a beverage project, and TRF engineering confirms the fit for each product, rate and plant. These are the ones that most often come up:
| Platform | Role at the end of the line | When it comes up |
|---|---|---|
| TRFIntraflow | Case conveying, accumulation, merging, diverting and elevation between machines | Conveying, accumulation and merging of cases and bundles between the packer and the palletizer |
| TRFSpeed | High-volume or multi-line palletizing, from a dedicated cell to a centralized system | High-rate lines and several lines feeding one palletizing area |
| TRFCompact | Industrial robot in a compact cell with a higher duty cycle than a cobot | Mid-rate lines that need an industrial cell in a compact footprint |
| TRFCobot | Collaborative palletizing for lower-rate lines, many SKUs and limited floor space | Smaller lines, short runs and plants with limited space at the end of the line |
| TRFOnepack | Erects, packs and seals the case in one machine | Lines that want case forming, packing and sealing in one machine |
| TRFRapidpack | Robotic, vision-guided case packing for flexible production lines | Packs that need robotic handling before they reach the case |
Capacity depends on the product, pack pattern and plant. TRF engineering confirms the final figures for each application.
Beverage projects and videos
TRF gathers projects and videos of applications in beverage and related segments. During the evaluation, the Sales Engineer shows examples that are close to your line, so you can see how similar steps were solved before you decide.
Questions
Frequently asked questions
Should Several Filling Lines Share One Palletizing Area or Each Have Its Own Cell?
It depends on line rates, plant layout and how often lines run at the same time. A centralized palletizing area can reduce the number of robots, but it needs conveying that merges and balances the flow. Separate cells keep lines independent. TRF compares both options with your real rates during the evaluation.
What Information Does TRF Need to Size a Palletizer for Cases and Bundles?
Send the case and bundle dimensions and weights, the target rate in cases per minute, the pallet patterns and sizes, the number of SKUs and the available floor space. Photos of the current end of the line help. A TRF Sales Engineer uses that list to match each step to a platform.
Can a New Palletizer Connect to the Stretch Wrapper and Equipment Already Installed?
Usually it can, and the connection is reviewed during the evaluation: pallet discharge height, conveyor interfaces and controls signals all matter. TRF plans the handoff so the new palletizer fits the line you already run instead of forcing a full replacement.
How Do You Compare a Manual Pallet Crew With a Robotic Cell?
Compare the labor hours per shift, the number of shifts and the local labor cost against the installed cost of the cell, including maintenance and electricity. Include the days when the crew is short. The palletizing ROI calculator gives a first estimate, and TRF refines it with your numbers.
Start your beverage packaging automation project
Beverage Packaging Automation works best when the case packer, conveyors and palletizer are chosen together, around your products, rates and floor space. Send your product list, package formats, case sizes, target rates and shifts, and a TRF Sales Engineer will map each step of your end of line to a platform.
Related industries: Food Processing, Consumer Packaged Goods, Distribution Center Automation. You can also compare the robotic palletizing, case packing and conveyor systems pages.
Next step
Keep your production running.
Tell us about your products, rates and floor space. A TRF Sales Engineer answers with the platform, the layout and the next step for your line.