Case Packing / Cup and Tub Case Packer
Cup and tub case packer matched to your line.
Pack cups and tubs into cases with the architecture that fits your product mix and line speed.
A cup and tub case packer is a top-load machine that picks filled, lidded cups and tubs from the line and places them upright into shipping cases in a set pack pattern. TRF Industrial Automation packs cups and tubs with TRFRapidpack and cups with TRFOnepack. The right one is defined mainly by your line setup and speed, not by the container alone.
Custom engineering
Solutions engineered for your production requirements.
Turnkey integration
From system design through installation and startup.
High reliability
Built for continuous operation.
U.S. support
Technical support for customers across the United States.
Lifecycle support
From startup to long-term performance.
What is a cup and tub case packer?
A cup and tub case packer is a secondary packaging machine that collates filled, sealed cups or tubs and loads them into a shipping case from above, in the count and pattern the case requires. It sits after the filler and sealer and before case sealing, conveying and palletizing.
The machine does three things in sequence. It receives the containers, usually in lanes from the filling and sealing line. It groups them into the layout the case needs, in one or more layers. Then it places the group into an open case, by robotic pick-and-place or inside an integrated machine that also erects and seals the case. All TRF case packers load from the top; the top load case packer page explains the format across the family.
Cups and tubs arrive at the end of the line in high counts and frequent format changes: single cups, multipacks, promotional packs and private label versions of the same product. Manual packing works until volume, SKU count or labor availability makes it the slowest step on the line. Cup and tub lines are common in dairy and cheese, frozen food and ice cream and food processing plants, including prepared foods.
How does a case packer protect cups, tubs and lid seals?
A case packer helps protect cups and tubs by picking them on surfaces that can take the load and placing them rather than dropping them. Cups and tubs are rigid enough to pick one by one or in groups, but a machine can only grip the lid, the rim and the sidewall.
- The lid is the seal. Picking on a foil or film lid has to hold the container without deforming the seal. Where the lid cannot take the load, the tool picks from the sides or supports the container underneath.
- Tapered walls. Most cups and tubs taper, so side gripping has to account for the angle and for how containers sit against each other in the case.
- Cold and condensation. Refrigerated and frozen containers can arrive wet or frosted, which changes how tooling grips them.
- Multipacks and sleeves. Banded, shrink-wrapped or sleeved multipacks behave differently from single cups and are treated as a separate format in the recipe.
- Label orientation. Retail-ready cases may need labels facing one way, which adds an orientation step to the pick and place.
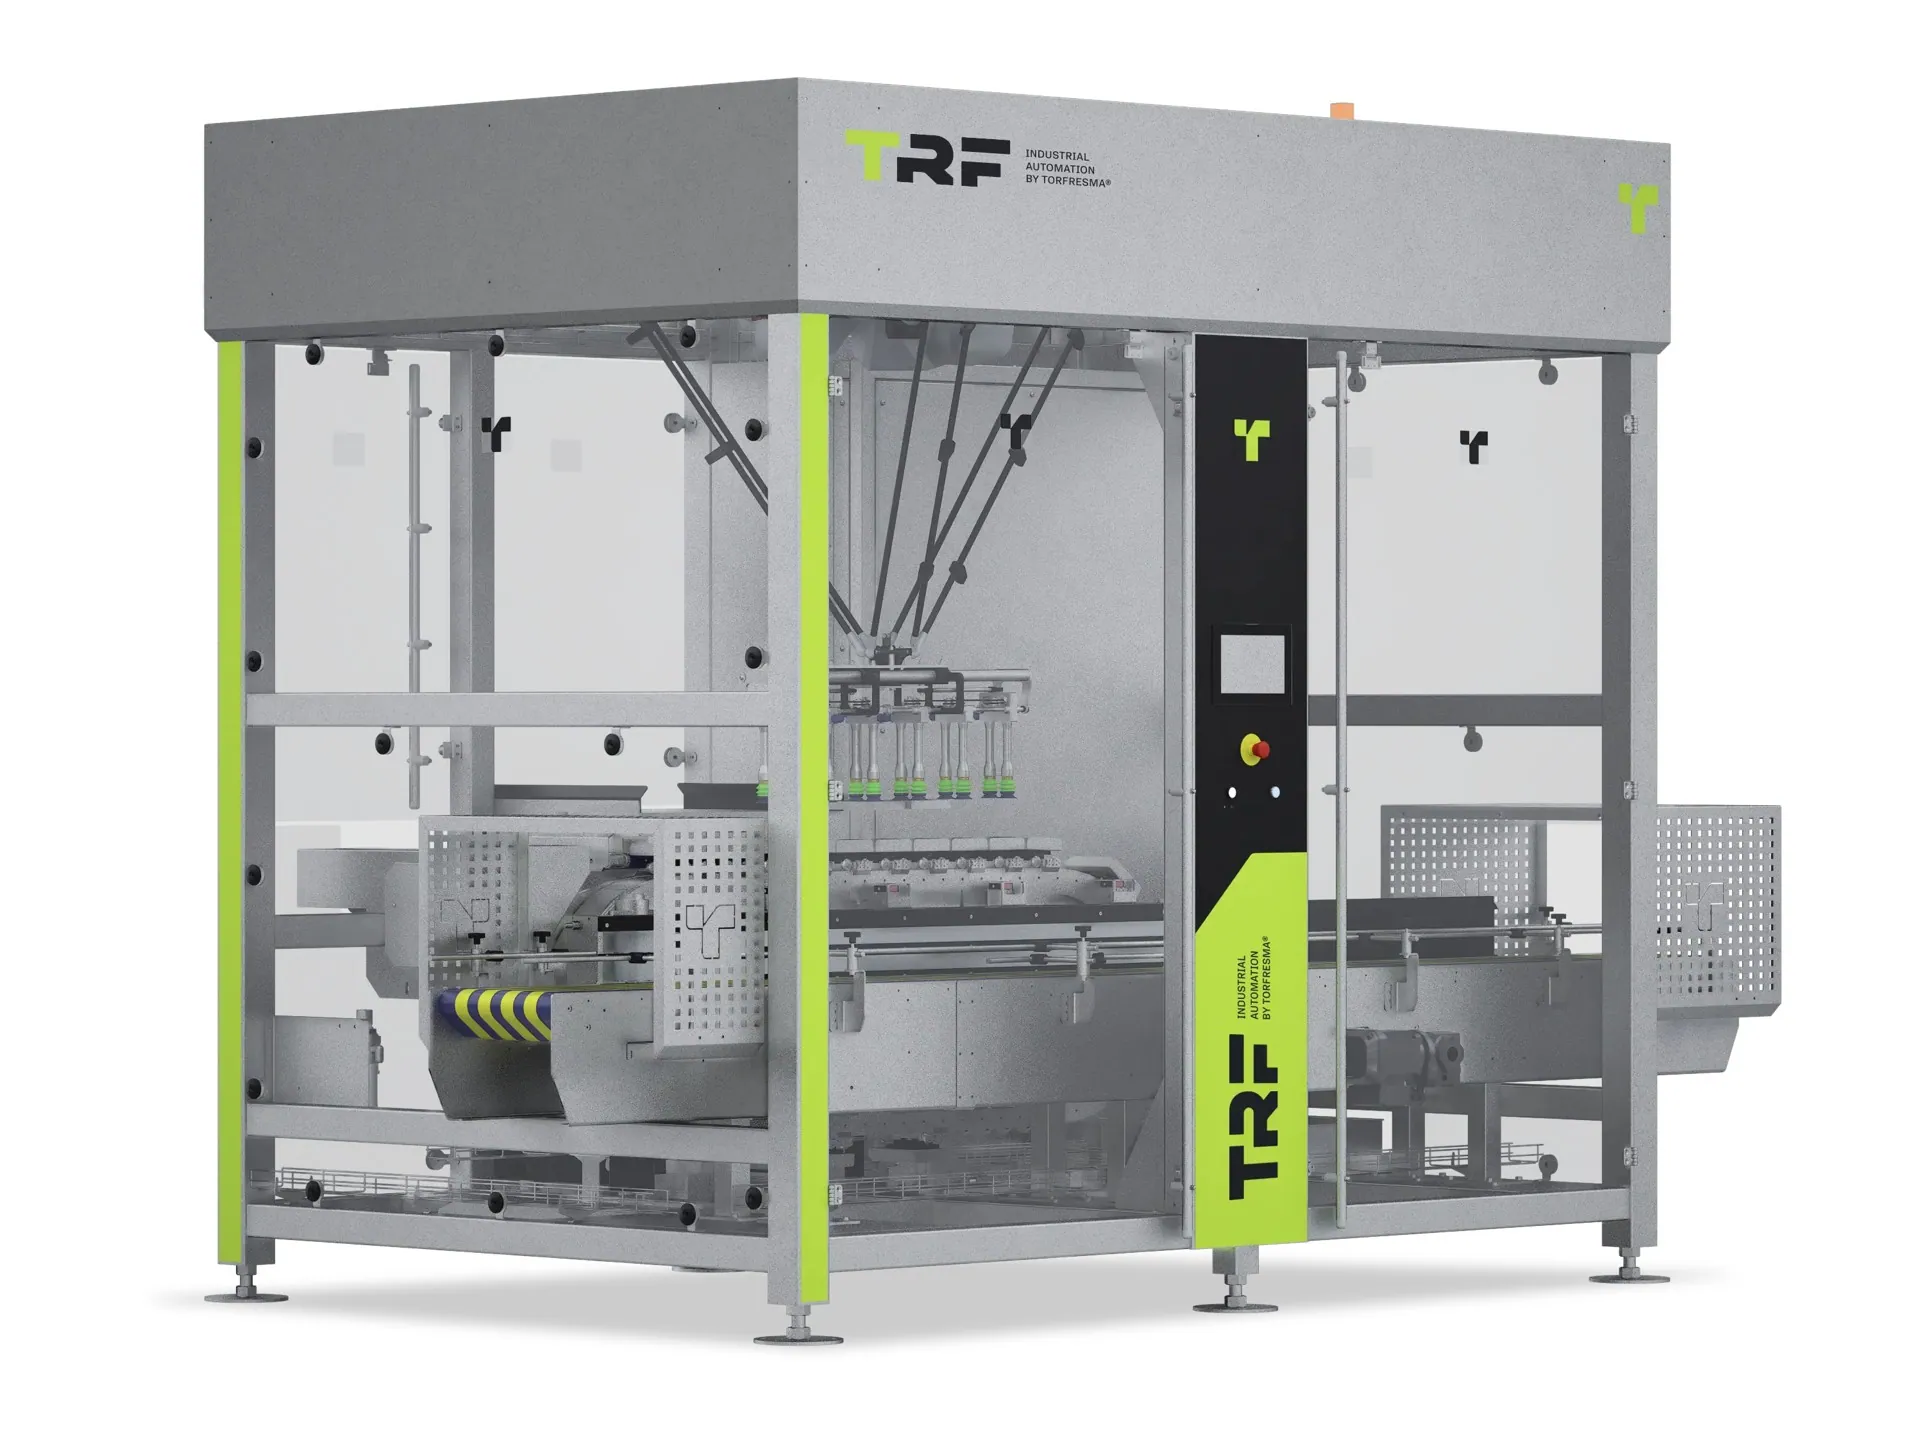
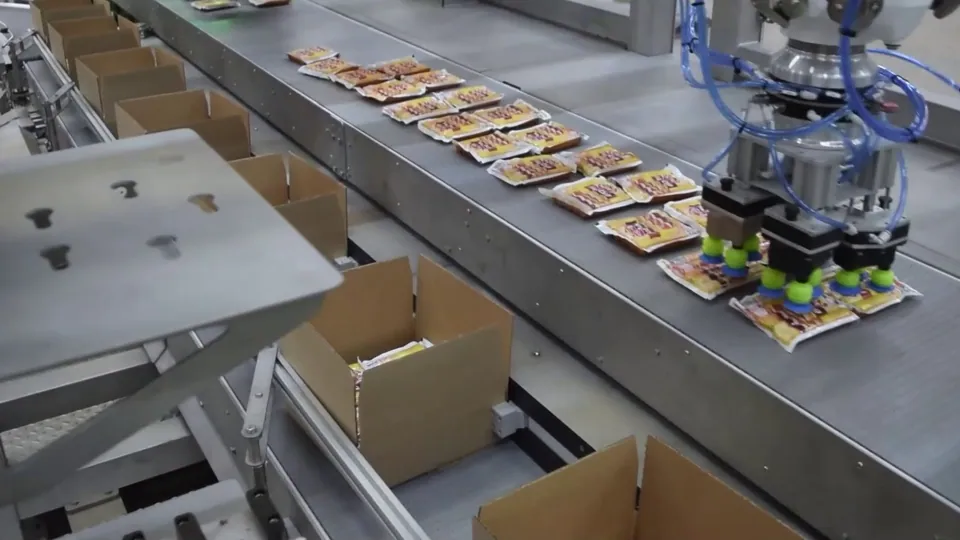
TRFRapidpack is designed for controlled handling of delicate, flexible or irregularly shaped products. TRF validates the tooling against your real containers, including cold product, before the machine is built.
How are cups and tubs packed into cases?
Cups and tubs are packed upright in a pattern defined by container size, case size, count per case and the number of layers. Retail-ready cases, club-store formats and e-commerce cases can use the same container with different patterns, and that is where changeover time becomes a real cost.
TRFRapidpack changes products and patterns by recipe, with reduced mechanical adjustments, so switching from one cup format to another is mostly a recipe selection plus any tooling change the containers require. TRFOnepack runs multiple products, recipes and packing patterns through robotic loading within the validated application. Each format is validated during project engineering.
Settle a few questions before the pattern is fixed: which counts per case you actually ship, whether pads or dividers go between layers, how the case is closed and whether a specific face must be visible on the shelf.
Which cup and tub case packer fits your line setup and speed?
Choose by line setup and speed. The three TRF case packing platforms form one family, and the right model is defined mainly by your product mix, how containers arrive, whether the case must be erected and sealed in the same machine and the products per minute you run.
| Line setup and speed | TRFRapidpack | TRFOnepack | TRFDroppack |
|---|---|---|---|
| Application range | For applications of about 100 to 200 products per minute | For applications of about 20 to 50 products per minute | For applications of about 20 to 500 products per minute |
| Packing principle | Delta robots, vision-guided or indexed | Erects, packs and seals the case in one machine | Controlled gravity loading |
| Cups and tubs | Cups and tubs | Cups | Not for cups and tubs |
| Line setup it fits | Many SKUs, variable product position, frequent changeovers | Replacing manual or semi-automatic packing, limited floor space | Repetitive flexible packages |
| Primary driver | Flexibility | Integration | Efficiency |
Application ranges for commercial screening, not machine speeds. TRF engineering validates final capacity for each application (container, end-of-arm tool, pack pattern and case).
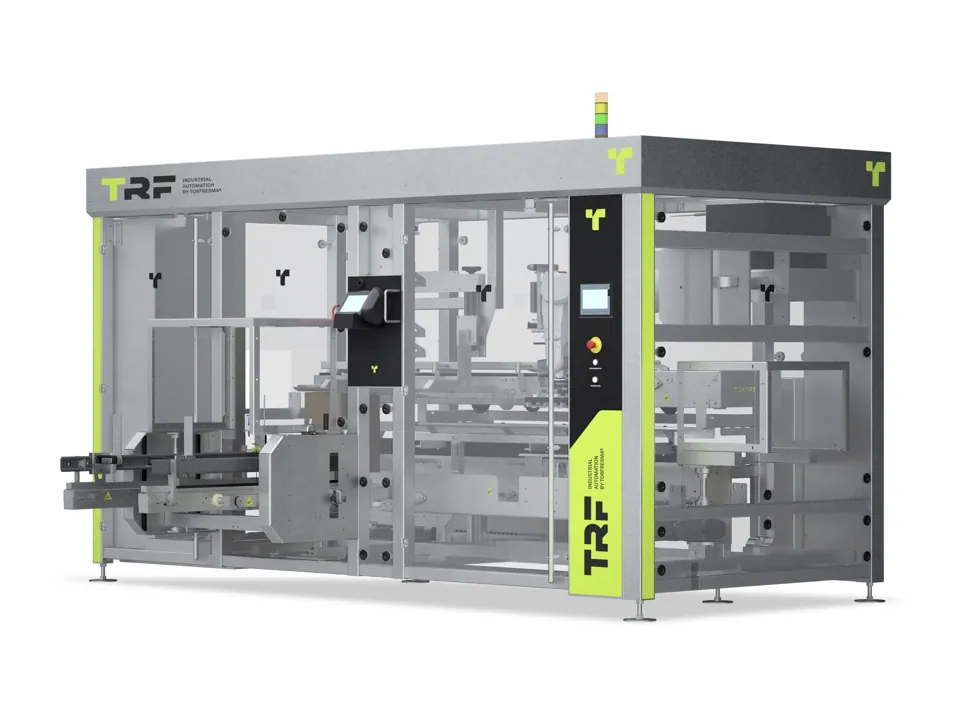
TRFRapidpack fits high-mix lines that run many cup and tub sizes, multipacks and private label variants, where product reaches the packer in variable positions. Recipe-based changeovers help keep format changes short, and the platform can grow from one robotic module to several.
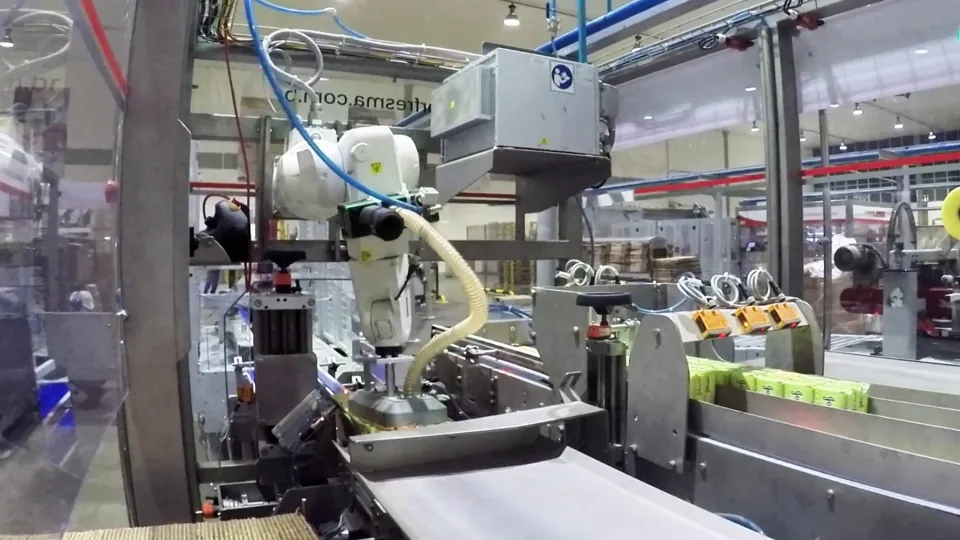
TRFOnepack fits plants where erecting, packing and sealing are separate steps today, or where floor space and equipment interfaces are the problem. It consolidates the three into one machine with one controls platform, for small and mid-sized food and CPG manufacturers.
TRFDroppack packs flexible packages such as bags and pouches, not cups or tubs.
Each platform can run standalone or as part of a complete TRF end-of-line system, with TRFIntraflow moving sealed cases to a TRF case palletizer. The case packing page compares the three platforms side by side.
Questions
Frequently asked questions
How Many Cups per Minute Can a Cup and Tub Case Packer Pack?
A cup and tub case packer from TRF packs cups and tubs in applications of about 100 to 200 products per minute with TRFRapidpack, or cups at about 20 to 50 with TRFOnepack, which also erects and seals the case. These are application ranges, not machine speeds. Capacity depends on the container, pick tool, pack pattern and sealer discharge, validated per line.
Does a Cup and Tub Case Packer Need a Vision System?
A cup and tub case packer needs a vision system only when container position varies on the infeed. When cups and tubs arrive in controlled lanes from the sealer, indexed picking is enough. When the flow is variable or several SKUs share the infeed, TRFRapidpack packs with vision-guided delta robots that locate each container before the pick.
How Much Floor Space Does a Cup and Tub Case Packer Need?
A cup and tub case packer needs floor space set by the case size, the pack pattern, the infeed lanes and operator access. Consolidation changes the answer most: TRFOnepack erects, packs and seals in one machine architecture, which takes less floor space than three machines in series. TRF places the machine in your floor plan, with infeed and discharge, during the application review.
Can a Cup and Tub Case Packer Handle Cold or Frozen Containers?
A cup and tub case packer can handle cold or frozen containers when the tooling is validated with real product at production temperature, because condensation and frost change how a gripper holds a lid or sidewall. Dairy, ice cream and frozen food are focus industries for TRFRapidpack. On the pallet side, TRFSubzero palletizes in areas below 32°F.
Can a Cup and Tub Case Packer Connect to My Filler and Palletizer?
A cup and tub case packer connects to your filler and palletizer when the signals, buffers and conveyor handoffs are engineered in the same project. TRF defines the interface with the filling and sealing line upstream and the handoff to a TRFCobot, TRFCompact or TRFSpeed palletizer, or one you already own, downstream. See end-of-line integration.
What Is the ROI of Automating Cup and Tub Case Packing?
The ROI of automating cup and tub case packing comes from comparing the installed cost with annual savings: packers per shift, shifts per day, local labor cost, cases the line can ship once manual packing stops limiting it, and damaged lids and dropped containers avoided. Frequent format changes favor recipe-based changeover. A TRF Sales Engineer builds the estimate with your data.
Start your cup and tub case packer evaluation
The right cup and tub case packer matches your line setup, your speed and the number of formats you run, and that decision is made with your containers. Send TRF container drawings or samples, lid type, SKU list, case counts, current and target products per minute and a drawing of the area. A TRF Sales Engineer validates the tooling, the pattern and the platform.
Want to see TRF installations first? Browse the TRF case studies.
Next step
Keep your production running.
Tell us about your products, rates and floor space. A TRF Sales Engineer answers with the platform, the layout and the next step for your line.